Casting Tolerance & Machining Allowance Calculator
Look up a dimensional tolerance by material and casting process, inspect the selected CT grade, and separate size variation from the stock needed for machining.
Scope: local process-to-CT recommendations, dimensional tolerance bands and machining-allowance tables. The original table edition is not recorded. Geometrical tolerance, draft angle, shrinkage compensation and automatic wall-thickness grade adjustments are outside this calculation.
How tolerance differs from machining allowance
A larger tolerance band allows more dimensional variation. More machining stock provides material to remove. These solve different problems: adding stock does not make the as-cast part more accurate.
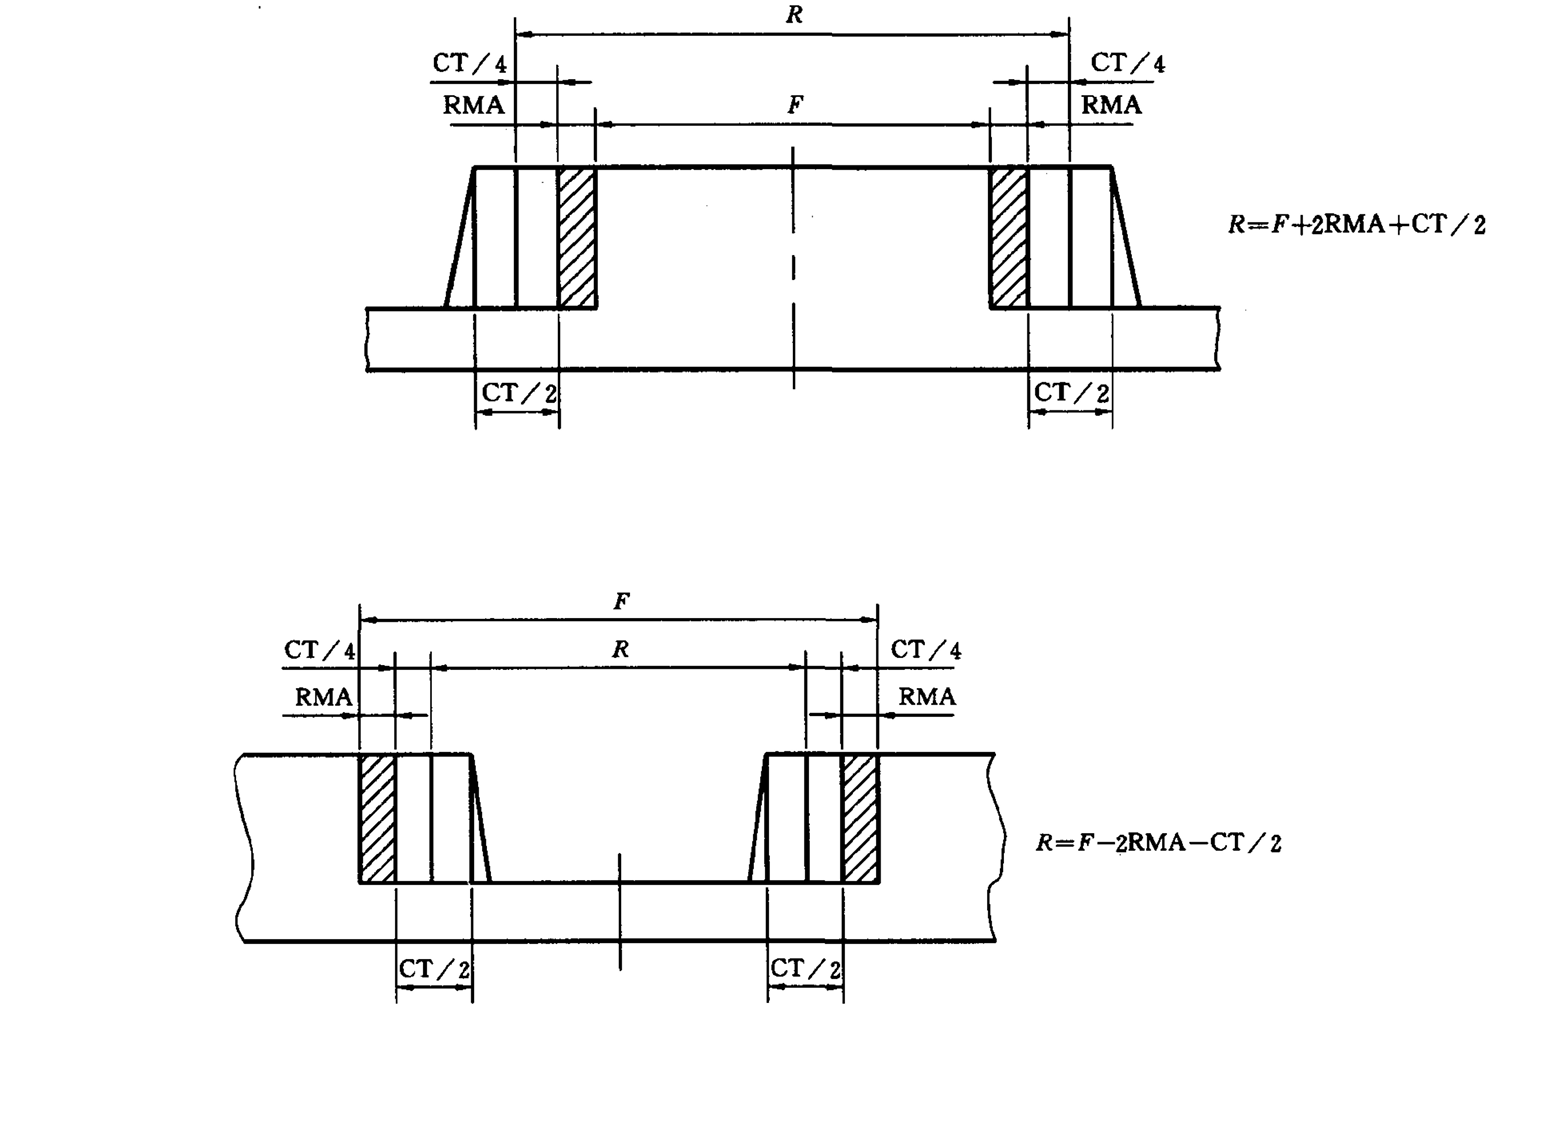
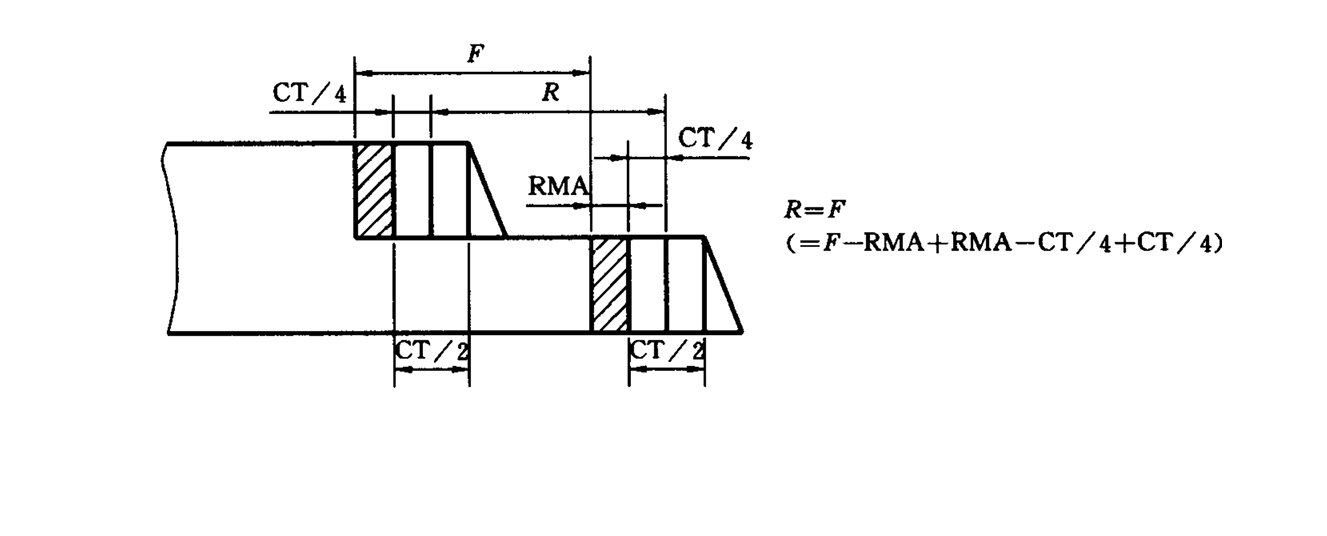
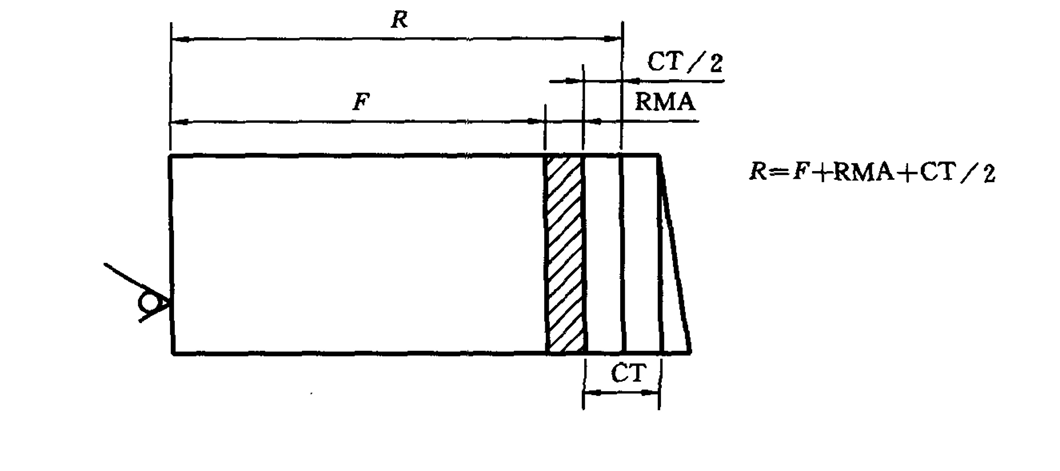
For an external feature, stock is added outside the finished faces. For a bore or cavity that will be machined larger, stock reduces the rough opening. A step or one-sided operation needs its own datum and stock plan.
Three worked local-table examples
100 mm nominal feature. Values checked against the local datasets and API on 2026-11-02; these checks do not certify a standard edition or a foundry’s capability.
| Material / process | CT allowance | Total band | RMA | Recalculate |
|---|---|---|---|---|
| Steel / manual sand mould | ±2.20 mm | 4.40 mm | 1.40 mm | Load example |
| Steel / silica-sol investment | ±0.20 mm | 0.40 mm | 0.70 mm | Load example |
| Aluminum / magnesium pressure die casting | ±0.20 mm | 0.40 mm | 0.30 mm | Load example |
In the first case the feature range is 97.80–102.20 mm. A 1.40 mm RMA does not widen that acceptance range. The three examples use different local process recommendations; they are not evidence that the processes are interchangeable.
When to machine or review the process
- Identify bearing seats, sealing faces and mating features that need machining; define datums and inspect the relevant features.
- Before tightening the CT grade, ask for evidence that the foundry can maintain it with the selected material, mould and production quantity.
- For wall thickness, draft or geometrical control, agree separate requirements; this calculator does not automatically change the grade or compute those checks.
- When stock is insufficient, a rough opening becomes non-positive, or a result is unavailable, review the geometry and allowance plan before quoting.
Sources and maintenance
Local data: process-to-CT recommendations, CT band records, RMA grades and allowance records. The original editions are not recorded. For the scope of the published standard, see ISO 8062-3:2023; this catalogue link does not establish that the local transcription matches that edition. Maintenance: Custom Parts Factory. Presentation/API version v1.1; revised 2026-11-02. Named engineering reviewer: not recorded.
Existing rough-dimension diagrams
F = final feature dimension; R = rough target; RMA = machining allowance; CT = total tolerance band.