Understand F-grade and E-grade dimensional limits for drop and vertical press steel forgings per EN 10243-1 — and calculate exact tolerances for your part.
Steel Forging Tolerance Calculator
Enter nominal size, weight, material group, and shape complexity to look up F-grade and E-grade tolerances per EN 10243-1.
From tolerance lookup to a manufacturing decision
Permissible tolerance is the allowed variation under the selected specification. Process capability describes variation demonstrated by a particular process, machine, material and inspection system. This calculator supplies a table lookup; it does not measure Cp/Cpk or guarantee a supplier can hold the limits.
This EN 10243-1 reference concerns steel drop and vertical press die forgings. It does not establish CNC finishing tolerances, an open-die forging specification or horizontal-upset capability. Confirm the applicable standard and delivery condition on the drawing.
Choose the dimension and shape factor
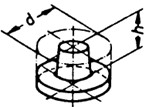
Illustration of an enclosing shape. Use the appropriate enveloping geometry for the forging, keep both masses in the same units, then select S1–S4. A ratio closer to zero means the forging occupies less of its envelope.Identify the measured feature and whether it crosses die halves. Length and thickness use separate rows; parting-line mismatch, draft and surface condition require separate consideration.
Worked lookup examples
Metric, vertical forging. Values below were checked against the local table entries and API on 2026-11-02. These are software/table consistency checks, not an independent certification of the original standard transcription.
Compact flange: For this 100 mm feature, the F band is 2.0 mm wide, not ±2.0 mm. Check the mating feature before accepting an as-forged fit.
Branched part, same size and mass: Changing only S1 to S4 widens the F dimensional band. The drawing should identify the chosen enveloping shape and support the complexity calculation.
Larger alloy-steel forging: Size, mass and material group all differ. F thickness is separately +3.3 / −1.7 mm here; do not copy the size tolerance onto thickness.
When to machine, change the process or request review
For bearing seats, sealing faces, locating bores and tightly controlled interfaces, compare the full tolerance band with the functional requirement. Plan finish machining and appropriate stock where the as-forged limits are too wide.
Before selecting a close grade, ask the supplier to confirm die condition, process control and inspection capability. A tighter grade alone is not capability evidence.
For thin webs, branches, dimensions across die halves or uncertain material/shape classification, review the drawing and feature definitions before using the lookup in an RFQ.
If secondary operations dominate cost, compare forging plus machining with another manufacturing route using the complete part geometry and batch quantity.
Sources, maintenance and next steps
Standard reference: BS EN 10243-1:1999, BSI catalogue. Implementation: CPF steel forging lookup tables; presentation model v1.1. Content and example check: 2026-11-02. Maintenance: Custom Parts Factory. Named engineering reviewer: not recorded. Confirm the licensed standard edition and any required corrigenda for contractual acceptance.
Closed-die steel forgings are shaped under high compressive forces in heated dies. Unlike CNC machining, final dimensions depend on billet size, die geometry, material shrinkage, flash trimming, and die wear. Standards such as EN 10243-1 (and the legacy German standard DIN 7526) define normal dimensional tolerances so engineers and buyers can specify realistic limits before quoting or machining stock allowance.
To determine applicable tolerances, you need the forging's largest nominal dimension, mass, steel material group, shape complexity category, applicable forging method, and whether F-grade (normal) or E-grade (close) limits apply. Use the calculator above to look up values from EN 10243-1 table data.
F-Grade vs E-Grade Forging Tolerances
F-Grade (Normal / Type F)
General-purpose tolerances for typical drop and vertical press forgings. Use F-grade when standard dimensional variation is acceptable and cost-effective production is the priority. Applies to length, width, height, thickness, and permissible deflection or distortion limits.
E-Grade (Close / Type E)
Tighter tolerances for precision forgings that must meet stricter dimensional control before finish machining. E-grade values are always narrower than F-grade for the same nominal size. Specify E-grade only where functionally required—it increases process control and cost.
Both grades are defined in EN 10243-1 Part 1 for drop and vertical press steel die forgings. Permissible deflection and distortion are expressed as symmetric ± limits based on nominal size bands (see table below).
Material Difficulty: M1 and M2 Steel Groups
High-carbon and high-alloy steels are more difficult to deform and cause greater die wear than low-alloy grades. EN 10243-1 assigns material groups that shift tolerance table rows:
Group
Carbon
Alloying Elements
Typical Grades
M1
≤ 0.65%
Mn, Ni, Cr, Mo, V, W combined ≤ 5% by mass
Most carbon and low-alloy steels (e.g. C45, 42CrMo4)
M2
> 0.65%
Mn, Ni, Cr, Mo, V, W combined > 5% by mass
High-carbon tool steels, high-alloy grades
Use the maximum permitted values from the steel specification to determine the group. M2 combinations with higher shape complexity (S3, S4) apply the largest table offsets.
Shape Complexity Factor (S1 – S4)
Thin sections, pockets, and branched geometries shrink unevenly and require higher forming forces, producing larger dimensional variation. The shape complexity factor accounts for this:
S = mf / mes where mes = l × b × h × ρ (ρ ≈ 0.00785 g/mm³ for steel)
mf = mass of the finished forging; mes = mass of the enveloping rectangular shape (length × width × height). The resulting ratio falls into one of four categories:
Category
S Factor Range
Interpretation
S1
0.63 – 1.00
Compact, simple shapes; lowest tolerance offset
S2
0.32 – 0.63
Moderate branching or thinner sections
S3
0.16 – 0.32
Thin webs, pockets, or multiple branches
S4
0 – 0.16
Highly branched or very thin sections; largest offset
In practice: divide the final part weight by the weight of the smallest box that fully contains the part. A solid cylindrical disk scores near S1; a thin-walled bracket with large cutouts may fall in S3 or S4.
Nominal Size and Forging Weight
Tolerance tables are indexed by two physical parameters:
Nominal size — the largest dimension of the forging (length, width, height, or diameter) in mm or inches.
Forging weight (mass) — the finished part mass in kg or lb, used with nominal size to select the correct table row for length/width/height and thickness tolerances.
Permissible Deflection and Distortion (by Nominal Size)
EN 10243-1 specifies symmetric ± limits for permissible deflection and distortion as a function of nominal size. Representative F-grade and E-grade values from our lookup data:
Nominal Size
F-Grade (±)
E-Grade (±)
≤ 100 mm
±0.6 mm
±0.4 mm
100 – 250 mm
±0.7 – 1.0 mm
±0.5 – 0.6 mm
250 – 630 mm
±1.1 – 1.6 mm
±0.7 – 1.0 mm
630 – 1250 mm
±1.8 – 2.2 mm
±1.1 – 1.4 mm
1250 – 2500 mm
±2.5 – 3.2 mm
±1.6 – 2.0 mm
Length, width, height, and thickness dimensional tolerances are separate table lookups that also depend on material group and shape complexity. Use the calculator for complete values.
Vertical vs Horizontal Press Forging
Vertical Forging (Drop / Press)
The most common closed-die process. EN 10243-1 Part 1 covers drop and vertical press forgings. Tolerance output includes length/width/height (F and E), thickness (F and E), and deflection/distortion (F and E). This matches the default mode in our calculator.
Horizontal Press Forging
Horizontal upset forgings fall under EN 10243-2. The examples and EN 10243-1 guidance on this page cover drop and vertical press forgings; do not apply them as a horizontal-upset specification.
Surface Roughness and Defect Limits
Beyond dimensional tolerances, forged surfaces typically require Ra values between 3.2 and 12.5 μm for as-forged condition. Sealing or bearing surfaces may require 0.8 – 3.2 μm after machining. Critical defects such as cracks and folds are not permitted; minor pits or pockmarks may be acceptable if depth does not exceed 50% of the machining allowance.
What is the difference between F-grade and E-grade forging tolerances?
F-grade (normal) tolerances apply to typical drop and vertical press forgings where standard dimensional variation is acceptable. E-grade (close) tolerances are tighter and used when the forging must meet more precise dimensional requirements—often before minimal machining. E-grade limits are always narrower than F-grade for the same nominal size.
Which standard defines steel die forging tolerances?
EN 10243-1 (Steel die forgings — Tolerances on dimensions — Part 1: Drop and vertical press forgings) is the primary European standard. It superseded DIN 7526 in many applications. Both define normal (F) and close (E) tolerance grades, material groups, and shape complexity factors used in tolerance lookup tables.
How is shape complexity factor calculated?
Shape complexity S = mf / mes, where mf is the mass of the finished forging and mes is the mass of the enveloping shape (length × width × height × steel density ≈ 0.00785 g/mm³). A ratio near 1.0 means a compact part (S1); thin or branched parts yield lower ratios (S3 or S4) and wider dimensional tolerances.
When should I specify M2 instead of M1?
Use M2 when the steel specification has carbon content above 0.65% or when the combined specified content of Mn, Ni, Cr, Mo, V, and W exceeds 5% by mass. High-carbon and high-alloy steels are harder to deform and cause greater die wear, so tolerance tables apply a larger offset for M2 combinations.
Do vertical and horizontal press forgings use the same tolerances?
Dimensional lookup tables differ by forging direction. Vertical press (drop) forgings typically have separate tolerance values for length/width/height, thickness, and permissible deflection for both F and E grades. Horizontal upset forgings require the separate EN 10243-2 specification; the worked examples here cover vertical forging.
How do nominal size and forging weight affect tolerances?
Tables are indexed by the largest nominal dimension of the forging and its mass. Larger dimensions and heavier parts generally fall into coarser tolerance bands because shrinkage, die wear, and thermal distortion scale with size. Enter both values when using the tolerance calculator for accurate results.
Standards Reference
Tolerance methodology follows EN 10243-1: Steel die forgings — Tolerances on dimensions — Part 1: Drop and vertical press forgings (also published as BS EN 10243-1). Historical German practice used DIN 7526 for similar normal tolerance grades. Calculator logic and educational content align with industry tolerance lookup practices for non-circular steel die forgings.